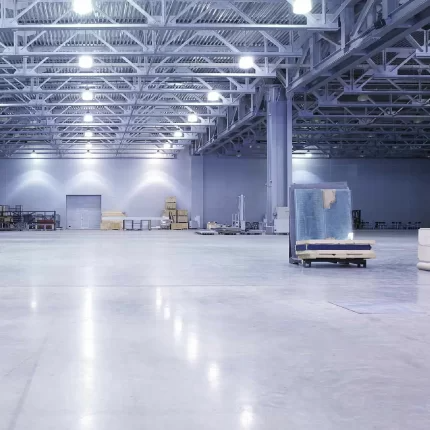
The Role of Epoxy Flooring Manufacturers in Industrial Safety
In the high-stakes world of industrial operations, where safety, efficiency, and durability are critical, flooring plays a surprisingly central role. While it may not immediately draw attention, the surface on which industrial activity occurs can significantly influence workplace safety and productivity. This is where epoxy flooring manufacturers step in, providing advanced flooring solutions that contribute immensely to industrial safety standards. From chemical resistance to anti-slip properties, epoxy flooring systems offer a comprehensive approach to creating safer environments for workers and machinery alike.
In recent years, industries have also started integrating complementary technologies such as polysulphide sealants in Dubai UAE to enhance the overall performance and longevity of flooring systems. These combined efforts ensure that industrial facilities not only meet but often exceed local and international safety regulations.
This blog delves into the vital role epoxy flooring manufacturers play in ensuring industrial safety and how modern innovations are transforming the way industries operate.
The Safety Challenges in Industrial Environments
Industrial environments present a host of safety challenges that vary depending on the type of operation. From manufacturing plants and warehouses to food processing units and chemical labs, each setting has unique requirements. However, some common flooring-related safety issues include:
1. Slippery Surfaces
Wet, oily, or dusty surfaces are major hazards in many industrial environments. Slips and falls can result in serious injuries and even fatalities.
2. Chemical Spills
Industries often deal with corrosive and toxic substances that can damage flooring and pose risks to health. If the flooring is porous or weak, it can absorb these chemicals, leading to long-term hazards.
3. Impact and Abrasion
Heavy machinery, forklifts, and constant foot traffic can wear down flooring quickly, creating uneven surfaces and trip hazards.
4. Temperature Extremes
Certain industries, such as cold storage and metalworking, operate in extreme temperatures, requiring flooring that can withstand thermal stress without cracking or degrading.
5. Fire Resistance
Fire safety is another essential requirement, especially in environments involving flammable materials. The flooring must resist ignition and contribute minimally to fire spread.
These challenges make it clear that industrial flooring must be more than just a flat surface—it needs to be a safety feature in itself.
How Epoxy Flooring Contributes to Industrial Safety
Epoxy flooring has gained popularity as a top solution for industrial settings due to its wide range of protective and performance-enhancing features. Epoxy flooring manufacturers design these systems with safety as a top priority. Here’s how epoxy flooring addresses the major safety challenges:
1. Slip Resistance and Traction
One of the primary benefits of epoxy flooring is its ability to offer excellent slip resistance. Manufacturers can modify the surface texture by adding aggregates or anti-slip coatings to increase traction. This dramatically reduces the likelihood of slip-and-fall incidents.
Moreover, epoxy can be tailored to meet OSHA and ADA slip-resistance requirements, making it an ideal choice for facilities aiming for compliance.
2. Chemical and Stain Resistance
Epoxy flooring systems are non-porous and highly resistant to a wide array of chemicals including acids, alkalis, solvents, and oils. This feature is especially crucial in pharmaceutical, chemical, and manufacturing industries.
Spills are easy to clean without risk of the chemicals penetrating the surface and creating long-term hazards. The flooring remains intact, maintaining a safe environment for employees.
3. Impact and Abrasion Durability
Heavy loads and constant traffic can degrade traditional flooring quickly. Epoxy flooring offers superior impact and abrasion resistance, which not only prolongs the life of the floor but also ensures that it remains smooth and even.
Uneven floors can be a tripping hazard and may also cause damage to machinery. By maintaining a level and durable surface, epoxy flooring contributes to both worker and equipment safety.
4. Thermal and Fire Resistance
Advanced epoxy formulations can withstand high temperatures and provide excellent thermal shock resistance. In environments with fluctuating temperatures, this prevents cracking or delamination.
Furthermore, epoxy flooring systems can be manufactured to be fire-resistant, significantly enhancing the overall fire safety of the facility.
5. Visual Safety Cues
Epoxy floors can be customized with different colors and markings for improved visibility and navigation. For instance, designated walkways, danger zones, and loading areas can be clearly marked on the floor.
This not only enhances operational efficiency but also minimizes accidents by guiding employee movements and vehicle traffic within the facility.
The Manufacturing Perspective: Innovation and Responsibility
Epoxy flooring manufacturers are not merely suppliers; they are innovators and safety advocates who take on the responsibility of ensuring their products meet evolving industry needs. Here’s a closer look at the manufacturing side of the story.
1. Formulating for Function
Modern epoxy flooring systems are engineered with precise chemical compositions to address specific safety concerns. Manufacturers spend significant time in research and development to enhance features like curing speed, VOC emissions, tensile strength, and chemical resistance.
The formulation phase also determines how well the flooring will bond with the substrate, resist moisture, and maintain longevity—all factors that impact safety.
2. Compliance and Certification
Manufacturers work in tandem with regulatory bodies to ensure that their products comply with national and international standards. Certifications related to slip resistance, fire safety, and environmental impact are crucial in gaining customer trust and passing safety inspections.
3. Collaborative Customization
Safety requirements often vary widely from one industry to another. Top manufacturers offer customized solutions tailored to specific environments—whether it’s anti-static flooring for electronics manufacturing or hygienic surfaces for food processing plants.
This ability to adapt to the client’s needs reinforces the role of epoxy flooring manufacturers as partners in safety.
4. Environmental Responsibility
In line with global sustainability goals, manufacturers are also exploring eco-friendly formulations. Low-VOC and water-based epoxies not only protect workers from harmful fumes during installation but also reduce the facility’s overall environmental footprint.
The Complementary Role of Sealants in Flooring Safety
While epoxy flooring provides a strong and resilient surface, its effectiveness can be enhanced further with the use of specialized sealants. One notable example is the application of polysulphide sealants in Dubai UAE, which are known for their flexibility and resistance to chemicals and weathering.
1. Joint Protection
Industrial floors often contain expansion joints that accommodate structural movement. Polysulphide sealants are used to fill these joints, ensuring they remain sealed even under stress or chemical exposure.
This helps maintain the integrity of the flooring system and prevents the infiltration of water, dust, or hazardous substances.
2. Edge and Perimeter Sealing
Where the epoxy floor meets walls, machinery, or drains, there are small gaps that can collect debris and bacteria. Polysulphide sealants provide a tight, hygienic seal, improving cleanliness and reducing safety risks.
3. Enhanced Durability
By sealing vulnerable areas, these sealants reduce wear and tear on the flooring system, extending its life and minimizing maintenance-related downtime.
Combining the robust properties of epoxy with the elasticity and chemical resistance of polysulphide sealants results in a more comprehensive and safer industrial flooring solution.
Key Industries Benefiting from Epoxy Flooring
The adaptability and protective qualities of epoxy flooring make it a preferred choice across various industrial sectors. Here are some industries where it plays a pivotal safety role:
1. Manufacturing and Warehousing
In environments where machinery, forklifts, and foot traffic coexist, epoxy flooring provides the durability and slip resistance needed to ensure safety.
2. Pharmaceutical and Healthcare
Sterility, chemical resistance, and easy cleaning are crucial in these industries. Epoxy flooring prevents microbial growth and supports contamination control.
3. Food and Beverage
Epoxy systems that meet FDA and HACCP guidelines help in maintaining hygiene, reducing slip hazards, and managing chemical cleaning agents.
4. Electronics and IT
Anti-static epoxy floors prevent electrostatic discharge (ESD), protecting sensitive equipment and reducing the risk of fire or malfunction.
5. Oil, Gas, and Chemicals
The need for chemical resistance, fireproofing, and spill management makes epoxy flooring a key safety measure in hazardous environments
Final Thoughts
The role of epoxy flooring manufacturers in promoting industrial safety is both foundational and forward-thinking. These manufacturers don’t just produce flooring—they engineer safety solutions tailored to the unique demands of modern industry. Through innovation, customization, and adherence to strict safety regulations, they help create environments that protect workers, preserve machinery, and minimize risk.
The integration of support materials like polysulphide sealants in Dubai UAE further enhances the safety and longevity of industrial flooring systems. Together, these materials form the backbone of resilient, compliant, and hazard-resistant industrial spaces.
As industries continue to evolve and safety standards grow ever more stringent, the partnership between facility managers and flooring manufacturers will be critical. Investing in high-performance flooring is not just a matter of aesthetics or durability—it’s a strategic move toward a safer, more efficient, and future-ready industrial operation.



Post Comment